Concrete mixer color changeover is complete only when the next saleable batch meets an agreed appearance requirement. An apparently clean vessel is insufficient: pigment can remain around the discharge, in the transfer hopper or in dosing equipment. Validate the entire material path with a defined dark-to-light transition, controlled water content and comparable cured specimens.
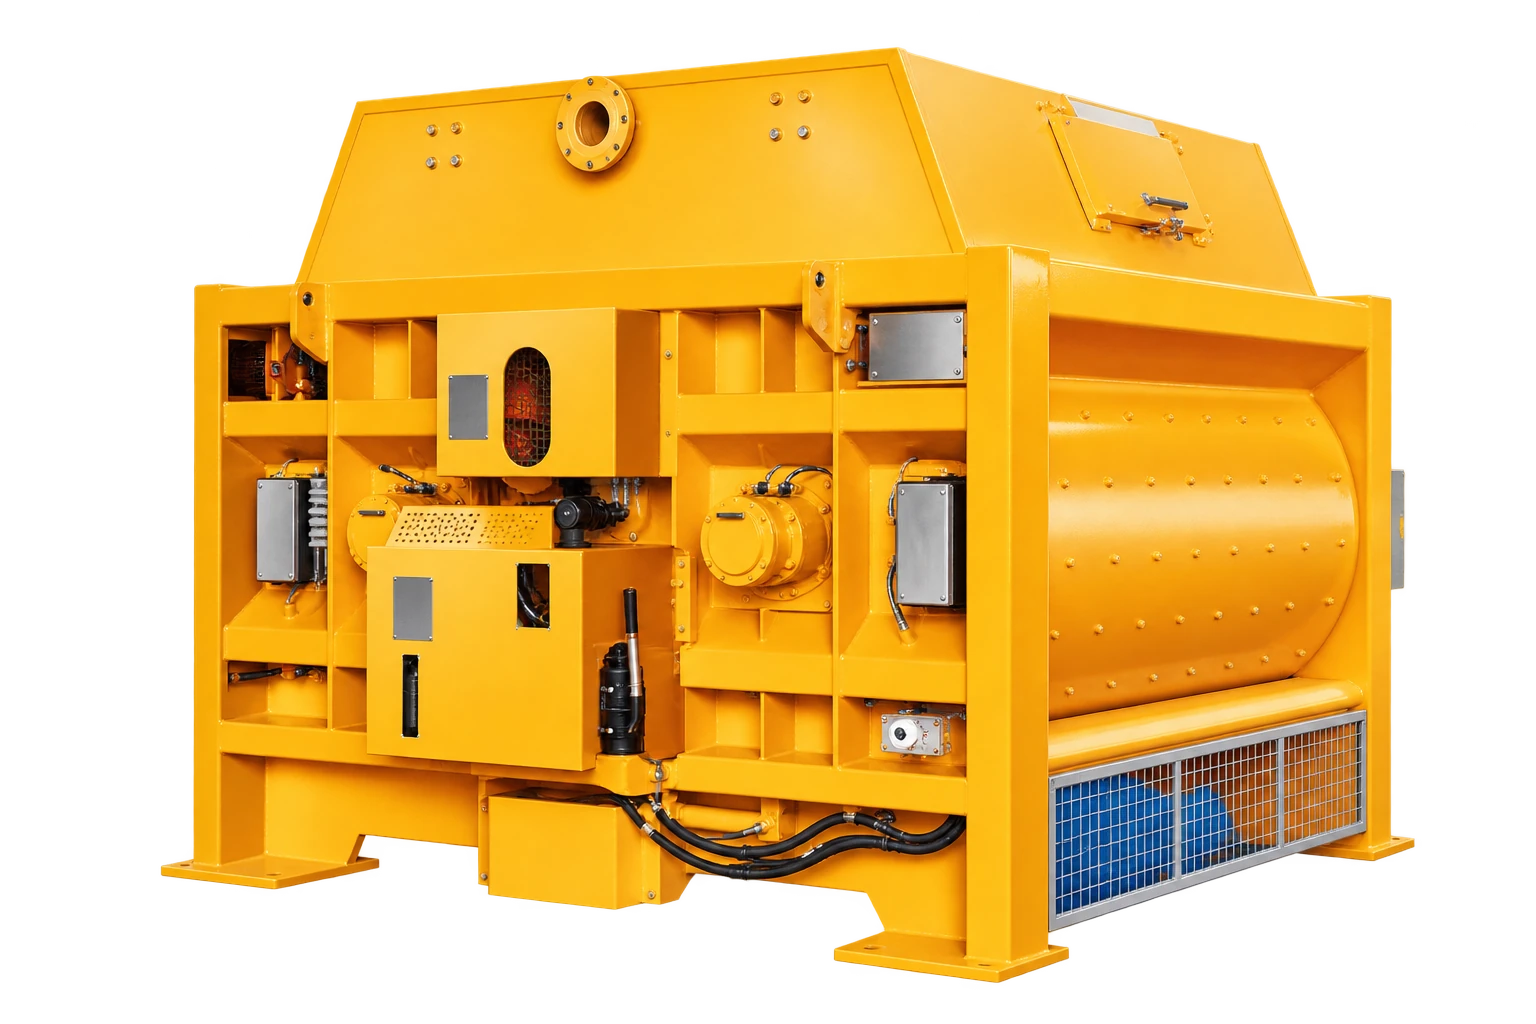
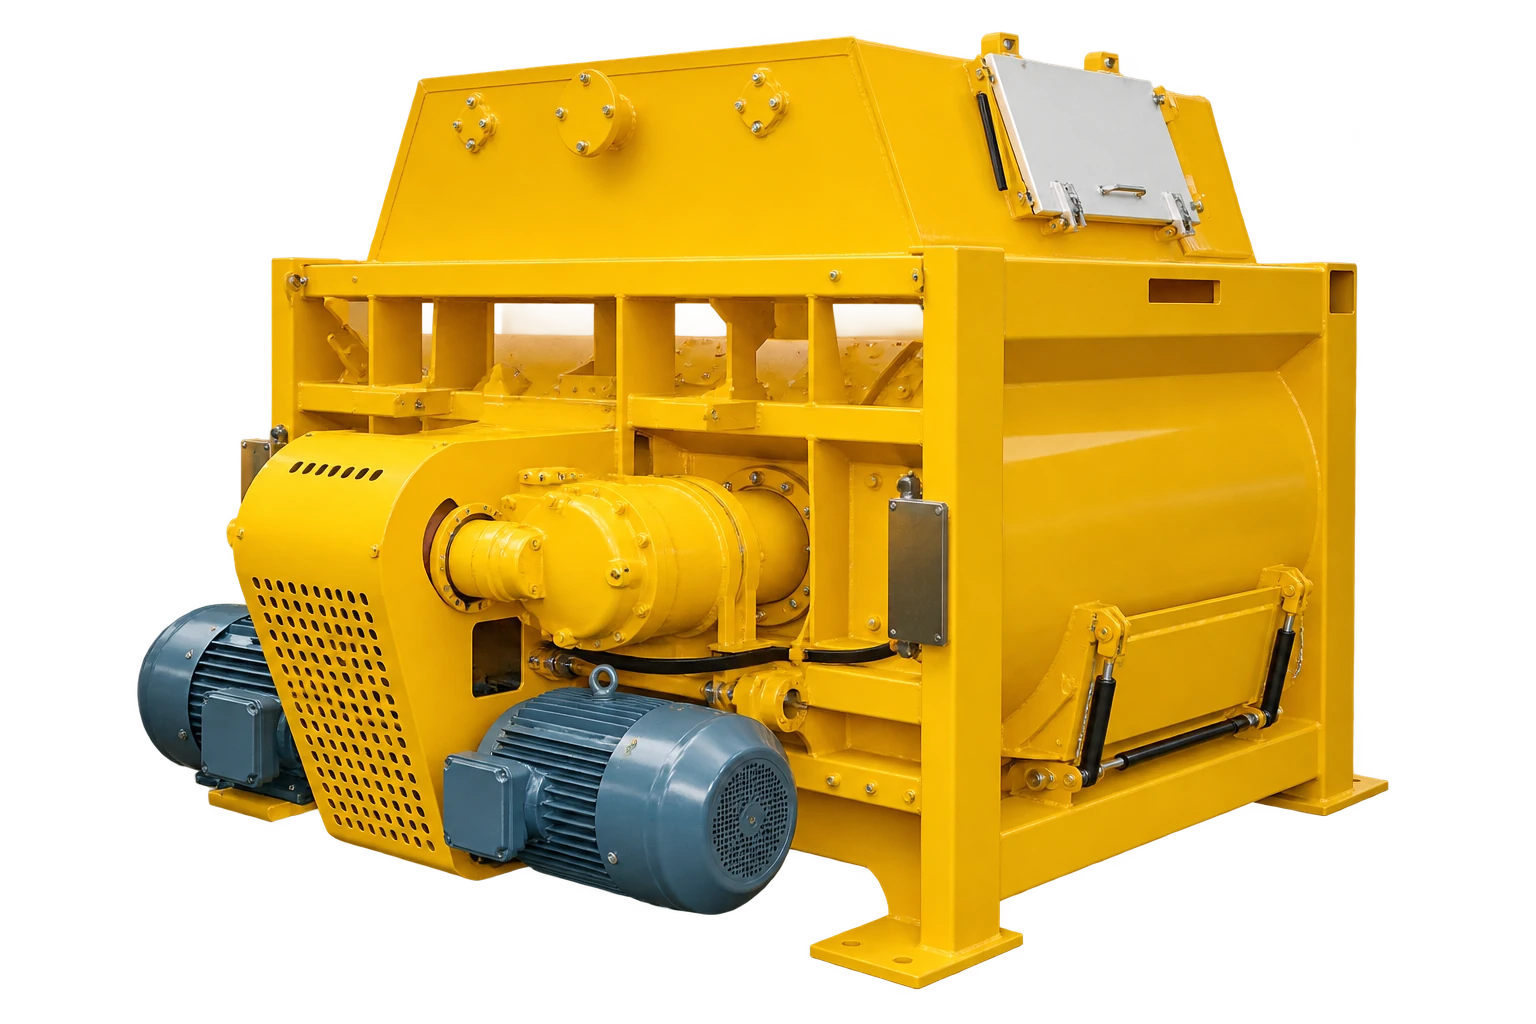
The MPO precast concrete mixer is a twin-shaft family for precast production. Its catalog selection basis is compacted output, mix design and production cycle. Cleaning configuration and access must be confirmed in the quotation; this article does not assert a standard automatic washing package or a guaranteed changeover time.
Define concrete mixer color changeover acceptance
First decide what “same color” means for the product. Face concrete, exposed aggregate and a smooth cast surface do not show color in the same way. PCI’s finish guidance identifies paste, sand and coarse aggregate as contributors, depending on exposure. Changing water can also change paste appearance.
Use a reference specimen approved for the actual surface finish. Define specimen age, curing, moisture state, lighting and viewing distance before the trial. A wet freshly cast coupon cannot be compared reliably with a dry mature panel. If instrumental color measurement is required, the project technologist must specify the method and acceptance band. Do not borrow a universal color-difference limit from another contract.
Keep a separate fresh-concrete acceptance check for consistency and discharge uniformity. A visually acceptable surface does not establish that water content, admixture dosing or concrete performance remains within the approved recipe.
Locate every possible carryover path
Inspect the process drawing from pigment dosing to mold filling. The mixer is only one hold-up location. List the pigment feeder, loading chute, lid, tools, shaft-adjacent areas, discharge gate, receiving hopper, conveyor and skip. A cleaned mixer can be contaminated again by the next item in that chain.
| Location | Evidence to collect | Decision |
|---|---|---|
| Pigment dosing path | Old material retained in screw, chute or container | Separate dosing-path purge from vessel cleaning |
| Mixing tools and walls | Deposits and inaccessible surfaces after discharge | Specify cleaning access and inspection points |
| Gate and outlet | Residue around edges, seals and closed pockets | Check gate position during approved wash sequence |
| Receiving hopper and transfer | Material retained before mold filling | Include downstream equipment in the trial |
| Water system | Remaining rinse water and drainage | Correct the next batch’s water balance |
This is a proposed engineering inspection map, not a claim that an MPO has every listed feature. Use the actual supplier drawing. Photograph repeatable points from a safe position so subsequent trials examine the same locations.
Plan the cleaning sequence and water balance
Discharge as specified, then use only the manufacturer’s approved cleaning method. Document automatic wash steps, drainage, any permitted manual work and the release check. BHS’s precast engineering page describes high-pressure cleaning as an option for frequent recipe changes. That is evidence of a design approach, not proof of its availability or performance on MPO equipment.
Ask the supplier which surfaces the jets reach, how nozzle blockage is detected and how discharge equipment is washed. The quoted pump pressure alone does not demonstrate coverage. Record the actual water used and the time to drain; a short spray cycle may leave a longer recovery operation.
Rinse water left in the vessel can change the following recipe even when pigment has been removed. Define how residual water is measured, removed or accounted for. Reused wash water requires a separate approved material-control procedure; do not add it simply because its color looks clear.
Screen carryover with a stated calculation
A simple mass fraction can help compare cleaning trials: carryover fraction = residual previous mix mass ÷ following batch mass × 100%. It is not a prediction of visible color, pigment concentration or concrete quality.
Hypothetical example: assume 4 kg of the previous mix enters an 800 kg following batch. The screening fraction is 4 ÷ 800 × 100 = 0.5%. If that same residue enters a 200 kg small batch, it becomes 2%. These are assumed masses, not MPO residue measurements or acceptance limits. The calculation explains why the smallest intended batch can be a demanding test.
Do not estimate pigment transfer by treating all old mix as pure pigment. Its composition and the retention location matter. Confirm appearance with the actual formulation and finished specimens; the mass calculation only identifies a case worth testing.
Run a dark-to-light verification trial
Choose a representative difficult transition rather than a convenient demonstration. Freeze the two recipes, raw-material lots, moisture correction, batch size and discharge route. Include any planned production break because material that dries during a delay may behave differently from fresh residue.
Run the dark recipe, discharge through the normal downstream path, perform the documented cleaning sequence and start the light recipe. Sample the start, middle and end of discharge using a safe approved method. Identify every specimen by batch and position. Make a control light batch on a separately verified clean path where practical, then compare specimens under the same curing and viewing conditions.
Record wash water, cleaning duration, drainage duration, residual observations and the first accepted light batch. If a sacrificial batch is needed, record its mass and disposition. Count it in the changeover cost instead of reporting only the washing time. Repeat the transition to establish whether the procedure works consistently.
The precast mixer selection guide addresses broader capacity and process trials. Keep this test focused on color carryover and release after cleaning rather than repeating general mixer selection.
Diagnose a failed trial before buying more washing equipment
An abnormal first sample that improves later suggests a localized retained-material path. Similar discoloration throughout discharge may require checking pigment dosing, aggregate lots, water correction and curing. Marks appearing only on finished surfaces can involve molds, release agent or finishing rather than the mixer.
Use those patterns to select the next inspection; they are clues, not proof of cause. Repeating the same wash with more water can hide a drainage problem or increase wastewater without resolving a contaminated receiving hopper. Change one controlled factor and compare with the original trial record.
For internal cleaning, OSHA’s energy-control guidance addresses unexpected startup and stored energy. The site procedure must govern access and release. An emergency-stop button alone does not authorize entry.
Conclusion
Concrete mixer color changeover needs a documented cleaning path and an appearance trial that can reject an unsuitable result. Include downstream residue, rinse-water control, the smallest batch and the first accepted product in the record. Use the verified procedure—not a claimed wash time—to compare cleaning options for the precast line.