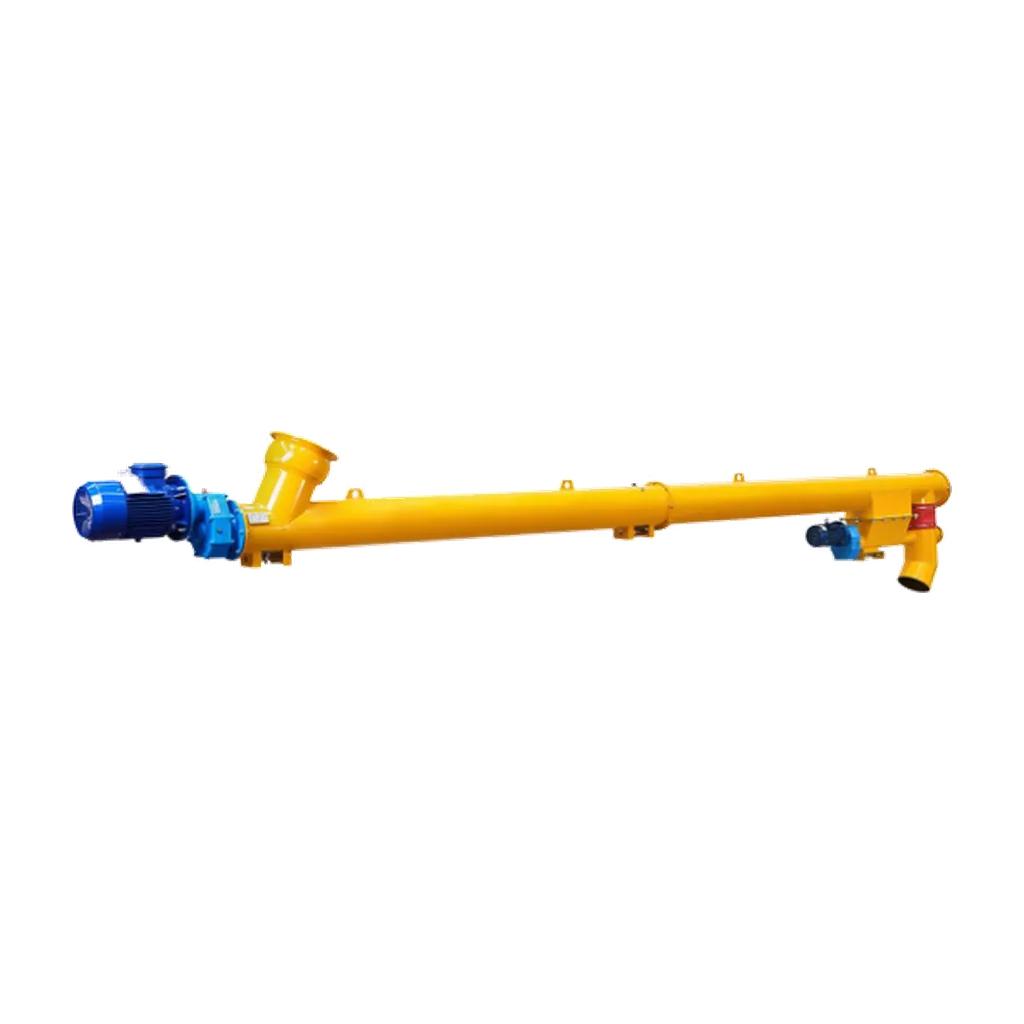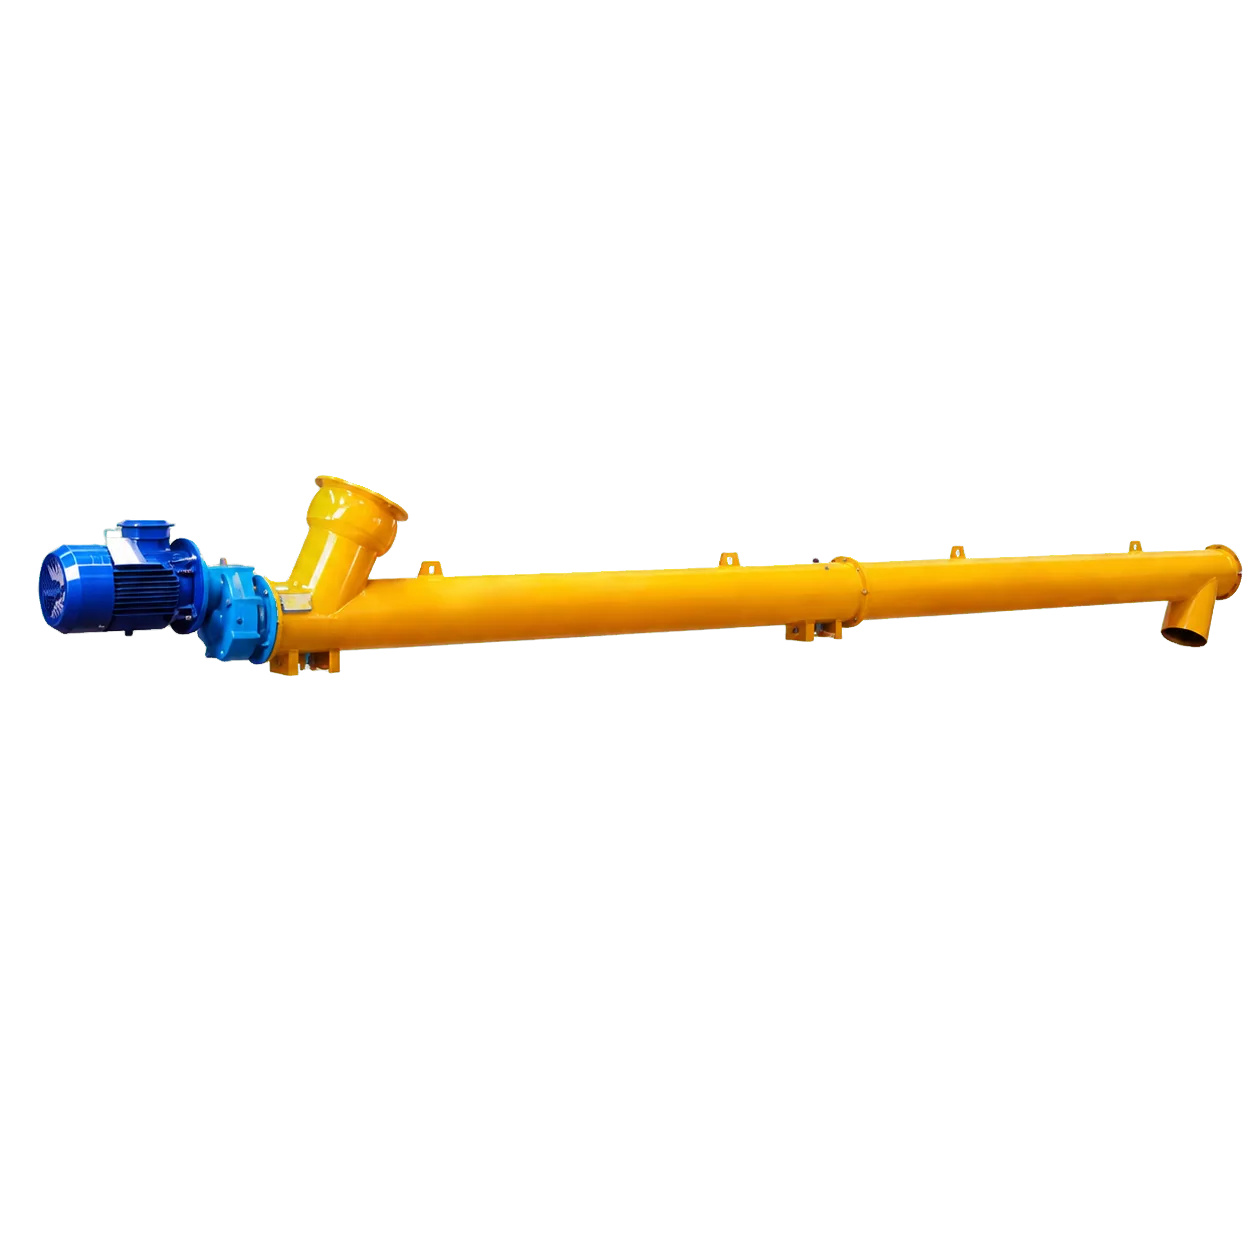
A blocked cement screw conveyor needs a check of the complete material path: silo outlet, inlet control, screw, discharge valve and receiving equipment. Moisture, surging feed, unsuitable geometry or mechanical resistance can produce similar symptoms. Repeated resets or a larger motor can worsen damage without removing the restriction.
For an enclosed cement screw conveyor transferring cement, fly ash or mineral filler to a weigh hopper or mixer, record what happened before flow stopped. Note material condition, valve status, motor load, speed and whether the machine stopped full. This distinguishes a true internal blockage from a silo that is not delivering or a receiver that cannot accept material.
Understanding the main causes of blockage
Moisture can promote sticking, agglomeration or hard deposits, but cement, fly ash and different fillers do not all behave identically. Check rain entry, condensation, wet compressed air and vapor from downstream equipment. Deposits around the shaft or hanger bearings reduce the free flow area; establish their source rather than assuming every restriction is due to ambient humidity.
Surges can exceed the usable capacity of a control-fed conveyor. If the inlet is continuously full beneath a silo, however, it is screw-feeder duty and needs a suitable extraction profile and loaded-start design. Merely slowing the conveyor with a VFD does not control uncontrolled gravity flow and may increase accumulation if upstream supply continues unchanged.
Pitch, diameter, speed and inclination must be considered together. Shorter pitch reduces geometric displacement at a given speed and fill, but can suit some feeder or incline arrangements. It is not automatically “too small” because of density alone. Gravity-driven fallback can reduce net delivery on an incline; 30° is not a universal limit for all cement screws. Confirm actual capacity and restart loads for the installed angle.
Drive problems can also stop movement. Check motor supply, protection settings, reducer ratio and mechanical torque limits, as well as the required running and starting torque. The catalog example of three-phase 380 V, 50 Hz, four poles and approximately 1,450 rpm describes a motor reference, not the screw output speed or proof of adequate power. Do not bypass an overload trip to force material through a restriction.
Identifying the location and upstream factors
Start with external indications and process records. A stationary silo inventory with little inlet delivery may suggest bridging or a stable flow channel; low delivery alone does not prove that the screw is blocked. Check actual valve position and the condition of installed flow aids. Aeration can help a suitable powder discharge, but excessive or wet air can create new problems. Hopper geometry, consolidation and feeder withdrawal must be considered together.
After safe isolation, inspect accessible inlet and internal locations for deposits, foreign objects, loose parts and rubbing. Wear does not always reduce clearance: loss of a flight edge usually increases its clearance, while a worn support can allow the shaft to sag and rub locally. Identify which dimensions changed instead of attributing every obstruction to “worn bearings.”
At the outlet, check valves, chutes, receiver level and vent filters. A closed valve, packed transition or full weigh hopper can back up an otherwise serviceable screw. A restricted vent may affect pressure and dust behavior; it is not evidence that increasing aeration will fix the problem. Locate the restriction before replacing the entire conveyor or drive.
Prevention and maintenance strategies
Coordinate upstream feed with verified downstream capacity and screw speed. A VFD is useful within the approved torque and speed range, but is not a substitute for a feeder or inlet shutoff where those are needed. In normal service, stop feed first and run out the screw when the process permits. Some silo feeders must start loaded, so design and validate that case instead of prescribing empty starts for every installation. Emergency stopping follows the safety function, not a compulsory runout delay.
On a suspected jam, stop the system and prevent further material entry. Before opening a hatch or clearing an obstruction, authorized personnel must apply the site energy-isolation procedure, control stored and gravity energy, verify isolation and secure any possible movement. An emergency stop or motor switch alone is insufficient. Settled powder can release suddenly and an inclined shaft may move backward. Do not reach into the conveyor, force repeated restarts or improvise a reverse-running sequence.
Select diameter, length, pitch and support arrangement for the material and duty. A tubular enclosure limits exposure but is not automatically airtight or pressure-rated. Increasing pitch can be part of a properly designed feeder extraction profile; it does not cure every compaction problem or replace hopper design. Published capacities are selection references requiring confirmation of fill, inclination and operating conditions.
Inspect hanger and end bearings, shaft alignment, flights, seals, couplings and supports using repeatable records. Suitable speed, level or load monitoring can detect an abnormal condition and trigger an agreed response. A reverse-pitch flight is a geometry feature, not a blockage sensor or a universal self-clearing device. Verify protection logic after relevant repairs and use the maintenance checklist to assign inspection tasks and responsibilities.
Conclusion
Prevent recurrent blockage by correcting the demonstrated cause across the silo, screw and receiver. Check moisture, feeding, geometry and mechanical condition together, then confirm stable operation and restart behavior. VOGO’s catalog selection diameters span Ø89–Ø407 mm; actual configuration depends on the project. Submit the blockage record and duty data with the conveyor datasheet for a configuration review.