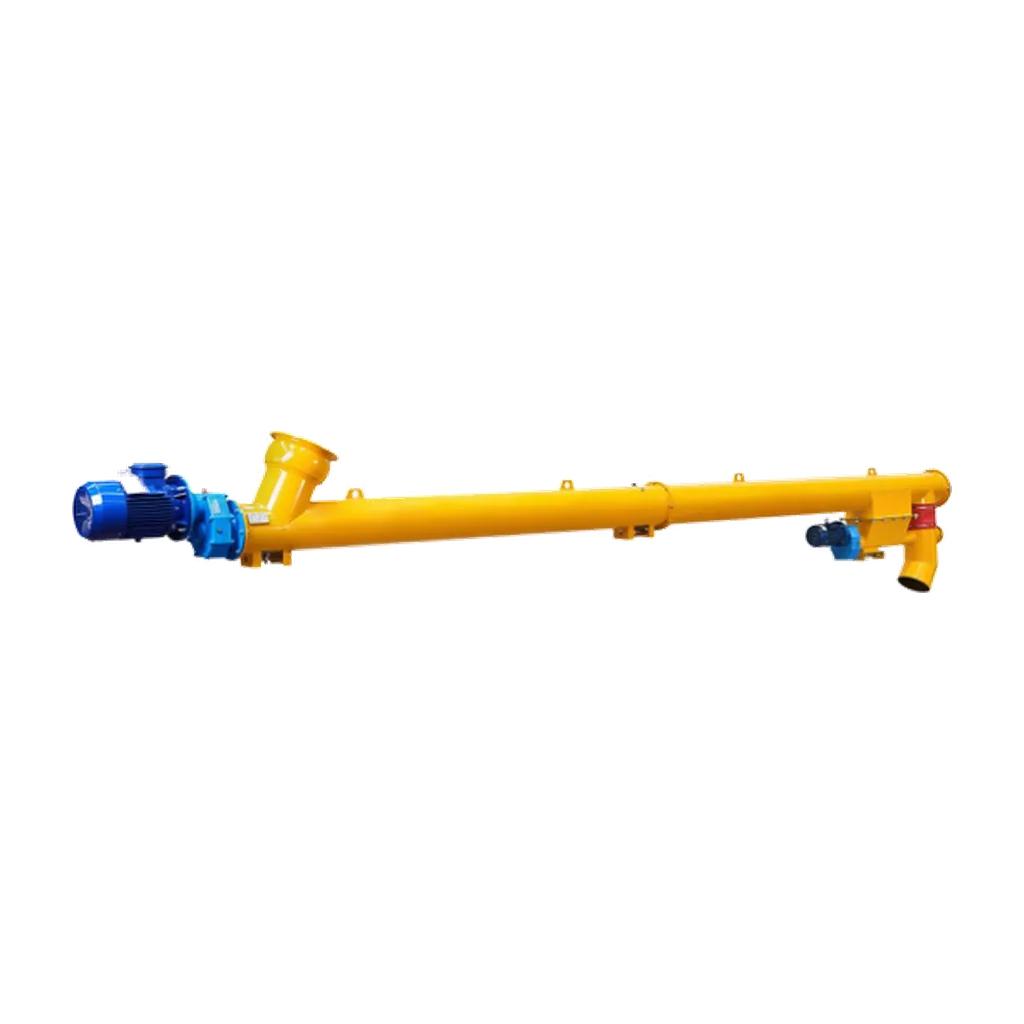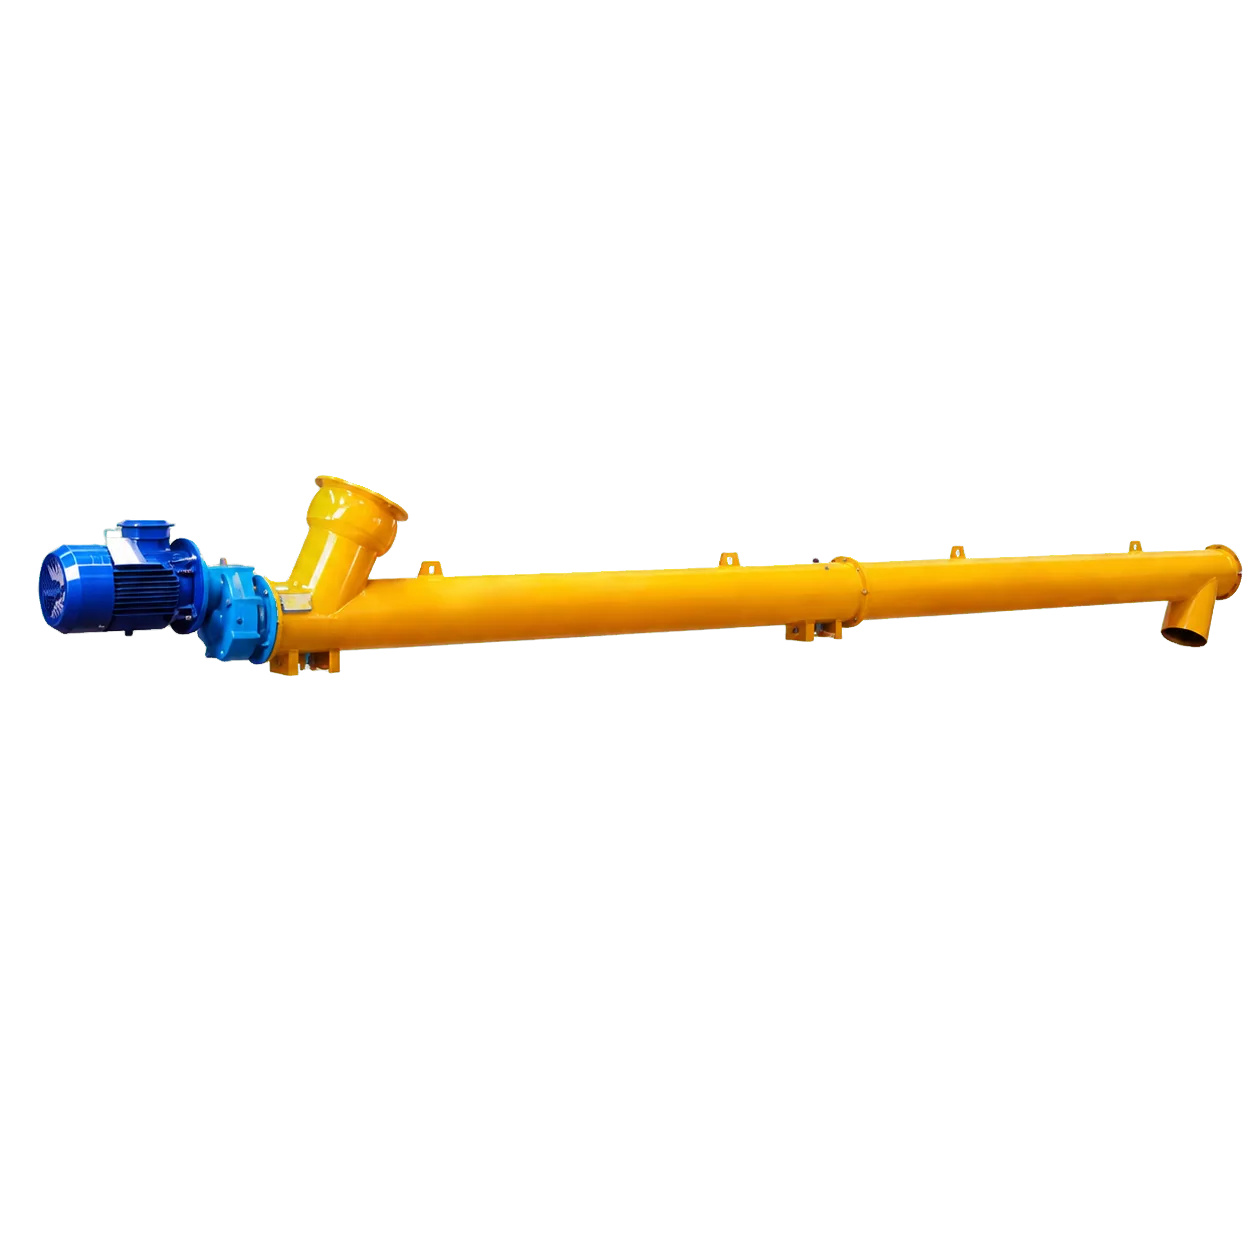
Calculate screw conveyor capacity in volume per hour first, then convert to mass using the material’s operating bulk density. Match the calculation to the actual screw geometry, speed, loading and inclination. For a tubular powder conveyor, an enclosed path can help contain dust and fit a compact layout, but enclosure does not establish delivery rate, airtightness or pressure capability.
The familiar Archimedes-screw principle is a useful starting point, not a guarantee that each particle advances one pitch per revolution. Real powder can slip, circulate, settle or retain air. A capacity estimate is therefore a selection input, and must be followed by checks of flow, power, mechanical loads and restart. This is especially relevant when batching cement, transferring dry mortar ingredients or feeding a chemical process within a limited cycle time.
Core variables governing screw conveyor performance
The main geometric and operating variables are screw outside diameter, centre-pipe diameter, pitch, screw speed and loading. Bulk density converts the resulting volume rate to a mass rate. A larger screw can permit a lower speed for the same required flow, but lower wear or less product damage must still be demonstrated for the material. Changing one variable can alter the acceptable range of others.
Lump passage requires its own check. Do not use universal limits of 25% of screw diameter for mixtures or 15% for all-lump material. The available space around the centre pipe, the largest lump dimension, hardness and proportion of lumps all matter. A soft agglomerate and a hard foreign object of the same size do not present the same problem. Consult the supplier’s applicable material and lump-size guidance.
Pitch is the axial spacing between corresponding points on successive flights. Standard, short and long pitch alter displacement per revolution; special flight shapes also affect transport. Shorter pitch can serve a purpose on an incline or in metering, but it reduces geometric volume per revolution at otherwise equal conditions. A long flooded hopper outlet requires a justified extraction profile, not merely a shorter constant pitch. The feeder-versus-conveyor guide explains this distinction.
The capacity formula and loading ratios
For preliminary screening of a shafted screw, use compatible SI units:
Qv = 60 × (π/4) × (D² − d²) × S × N × φ
Qm = ρ × Qv
D and d are the screw and centre-pipe outside diameters in metres; S is pitch in metres; N is screw speed in rpm; φ is the assumed occupied fraction of the annular area in this simplified model. Qv is m³/h, ρ is t/m³ and Qm is t/h. The factor 60 converts minutes to hours. This geometric estimate does not include verified allowances for slip, flight details, inclination or restrictions. It is not presented as the complete ANSI/CEMA 350 calculation method.
Hypothetical example: D = 0.300 m, d = 0.090 m, S = 0.300 m, N = 80 rpm, φ = 0.30 and ρ = 1.2 t/m³ give Qv ≈ 27.79 m³/h and Qm ≈ 33.35 t/h. These are calculated values, not a VOGO rating. If operating density falls while delivered volume stays the same, mass flow falls proportionally. Capacity and drive loading must therefore be reviewed against the relevant density extremes rather than one convenient average.
Manufacturer tables may define trough loading differently from this annular-area assumption and may already incorporate standard geometry. Use a consistent method. Do not apply a table factor to this formula without checking its definition, or multiply the same correction twice. KWS’s public capacity guide explicitly separates control-fed conveyor tables from flood-loaded feeder design. Its maximum table speeds are also not recommended operating speeds for every material.
Loading is selected for the particular powder, abrasiveness, flow behaviour and equipment. Values such as 15%, 30% or 45% appear in engineering tables, but assigning universal 12–15%, 25–30% and 40–45% bands solely from a verbal flowability label is not a sufficient design rule. Use properties at the conveyor inlet, including aeration, moisture and consolidation, rather than assuming upstream test conditions remain unchanged.
Accounting for inclination and operational risks
Inclination can cause fallback and reduce useful output. The correction depends on the material, speed, flight geometry and housing. Generic factors of 0.9 at 5°, 0.8 at 10° or 0.65 at 20° should not be treated as universal or as verified VOGO data. If a supplier supplies a factor C, first establish whether it reduces delivered capacity or increases the selection requirement, and which configuration it covers.
For example, a hypothetical delivered-capacity factor C = 0.80 would turn a 25 m³/h requirement into a base selection requirement of 25/0.80 = 31.25 m³/h. This only illustrates factor direction, not an inclination recommendation. A factor already included in a supplier’s rated table must not be applied again. Changes to pitch or housing require a fresh check of both retention and geometric displacement.
Power and startup are separate from steady capacity. Check the allowed material inventory at shutdown, possible consolidation, upstream head load and the torque available at the screw. A drive that sustains normal transfer may not restart the specified loaded condition. Reducer, shaft, couplings and protection must suit that load path; a larger motor alone does not establish adequacy. Agree on whether an abnormal blockage must be cleared under isolation rather than overcome by motor torque.
Practical selection and project-specific configuration
Provide normal and peak flow, delivery time, density range, moisture, particle and agglomerate sizes, temperature and material safety information. Add centreline length, elevation, inclination, inlet and outlet drawings and connected-equipment pressures. State whether the inlet is controlled or flooded, whether service is continuous or metered, and the required starting frequency and restart state. These inputs make a supplier’s capacity claim reviewable.
Confirm electrical supply and actual output speed. A 3-phase 380 V/50 Hz motor is a catalogue reference; it must match the site, and motor rpm is not screw rpm after reduction. Abrasive or hot duties may need different construction, bearing arrangements or thermal allowances. Hanger bearings are not automatically appropriate in every short feeder or sensitive product. Define maintainable access and containment without assuming a closed tube is dust-free.
VOGO lists selection diameters from Ø89 to Ø407 mm and reference capacities from 1.3 to 170 t/h. The range spans different configurations and conditions; it is not one machine’s guaranteed operating range for every powder. Confirm the exact geometry and the meaning of the stated diameter, together with measured or validated capacity for the project.
Conclusion
Keep the capacity calculation, its units and its operating assumptions together. Confirm the chosen size through an agreed selection method and, where needed, a material trial; separately verify power, strength and loaded restart. For configuration data and a project review, use the cement screw conveyor page and datasheet.