Select screw diameter by converting the required mass flow into volume flow, choosing a material-appropriate speed and loading, then checking a supplier’s capacity data for the actual geometry. Diameter alone does not determine power or guarantee performance. Too little capacity can create a bottleneck; a larger machine may increase cost and space requirements, but can also permit a lower operating speed. The choice should be justified for the complete duty.
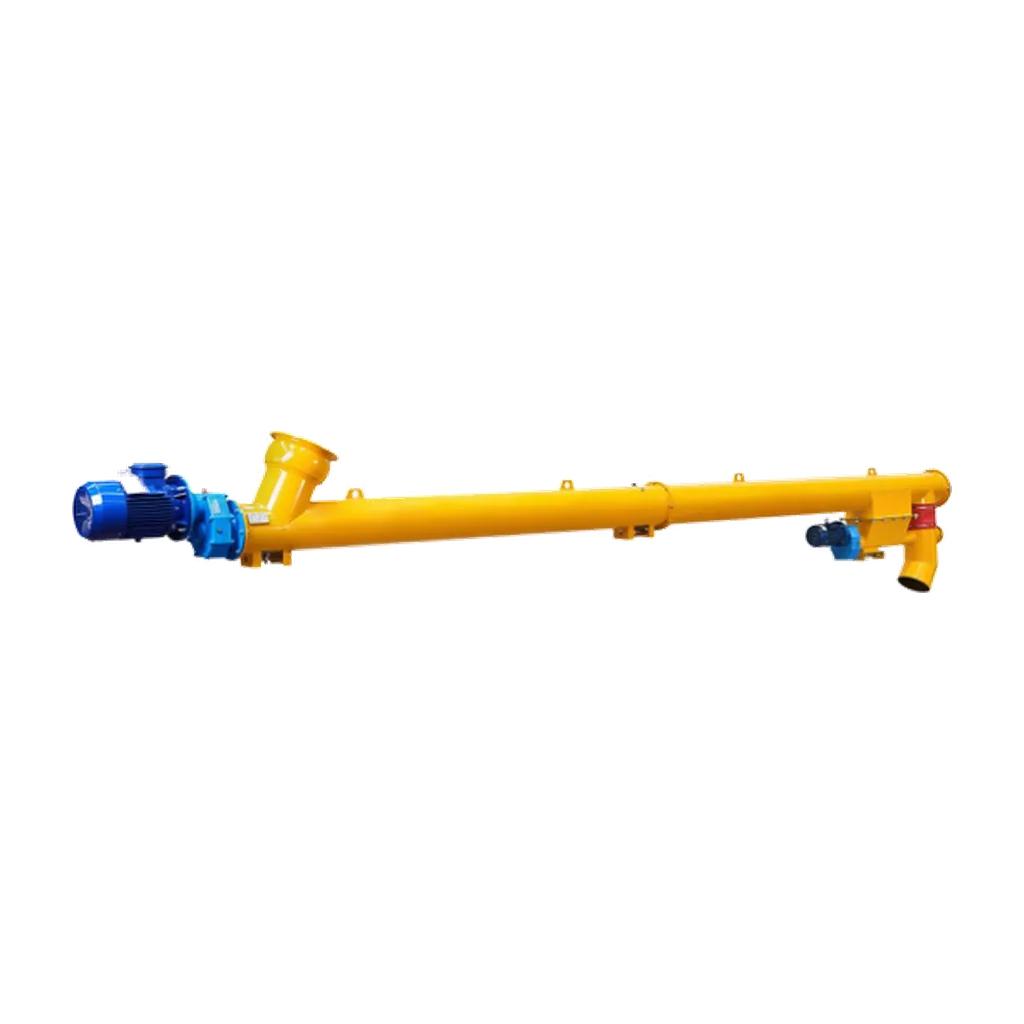
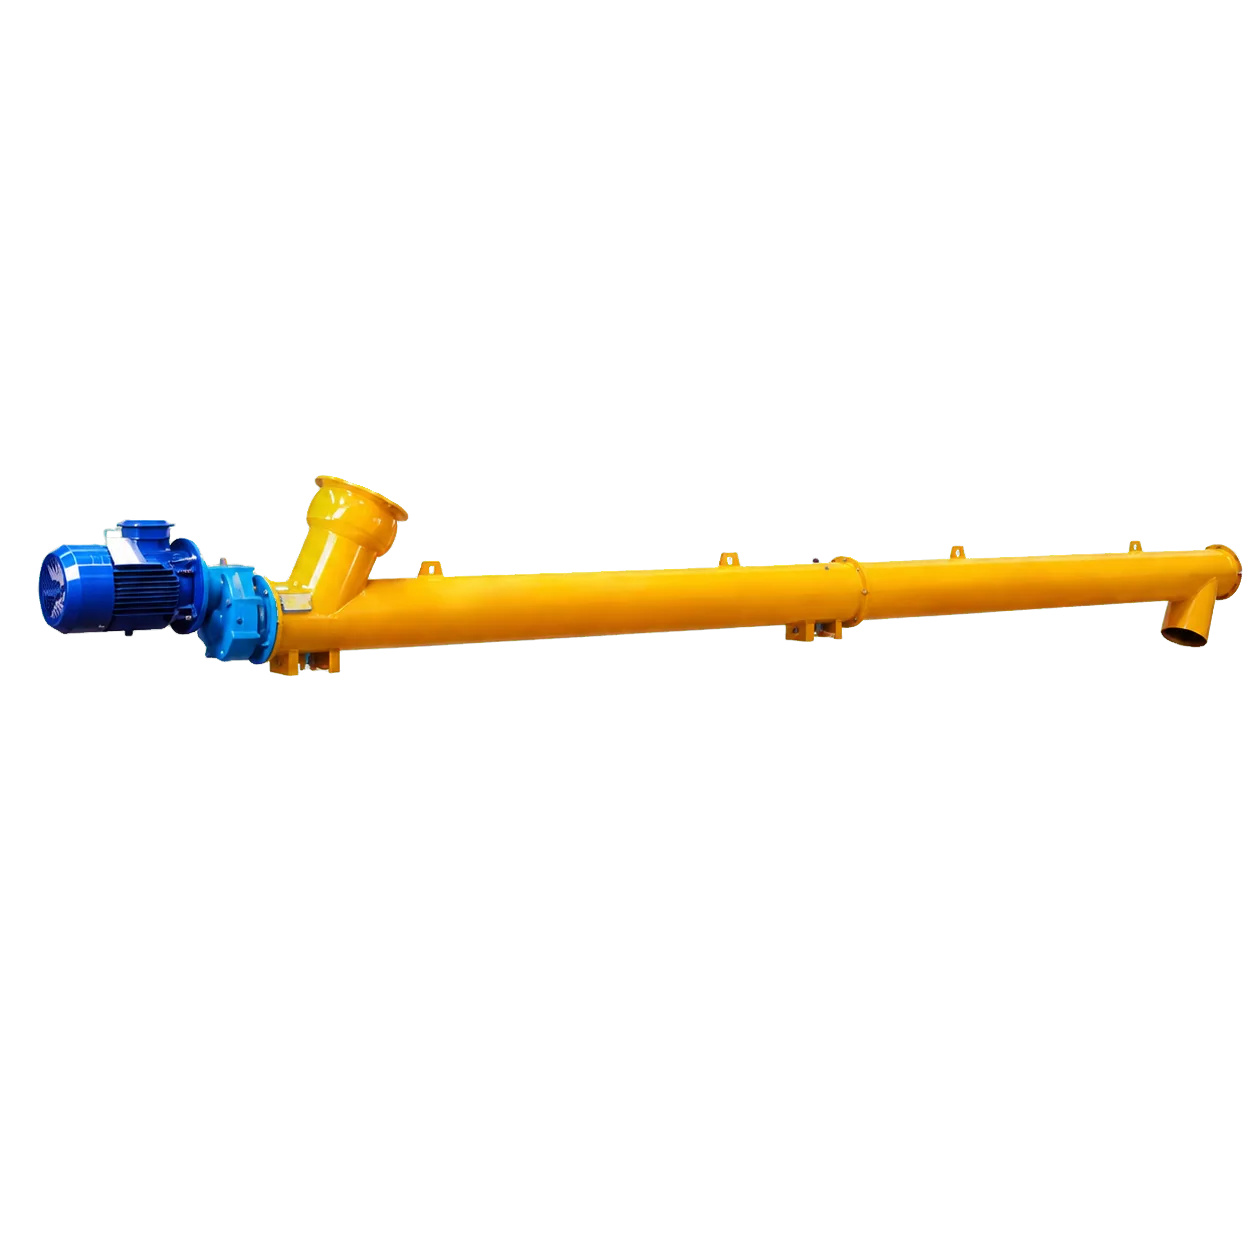
For cement batching or dry-mix mortar, the VOGO tubular screw range provides catalogue sizes to compare after establishing those requirements. Confirm whether its quoted diameter means screw outside diameter or tube diameter before inserting any catalogue number into a calculation. These dimensions are not interchangeable.
Project input checklist
Gather the following before sizing:
- Material and grade, operating bulk-density range, particle distribution, largest agglomerate, moisture, abrasiveness and flow behaviour.
- Normal and peak throughput in t/h or m³/h, including the delivery time allowed within a batch cycle.
- Centre-to-centre conveying length and the required elevation change.
- Inclination measured from horizontal, with sufficient layout information to check the angle.
- Inlet and outlet sizes, positions, connected equipment and pressure conditions.
- Continuous transfer or metering duty, and especially controlled feed versus direct extraction below a flooded hopper.
- Ambient and material temperatures, relevant dust classification, supply voltage and frequency; 3-phase 380 V/50 Hz is a catalogue example, not a universal requirement.
Material conditions and their effect on diameter
At a fixed mass rate, lower bulk density means greater required volume, not the reverse. Higher density may increase loading and drive demands for a given filled volume. Check both effects separately. Particle size and the proportion of hard lumps also constrain passage around the centre pipe. A larger diameter does not independently cure a cohesive arch in the hopper or an unsuitable outlet.
Do not adopt 1.2–1.5 t/m³ as a guaranteed range for every cement or similar powder. Use measured states at the conveyor inlet, including aerated and settled conditions where relevant. Aerated powder may flow readily but also flush uncontrollably; settled powder may consolidate during a stop. Neither behaviour is captured by merely labelling the material “free flowing.” Confirm speed, loading and restart requirements for the relevant states.
Diameter-to-capacity relationship and calculation steps
A preliminary geometric model for a shafted screw is:
Qv = 60 × (π/4) × (D² − d²) × P × n × φ
Qm = ρ × Qv
Here Qv is volume flow in m³/h; Qm is mass flow in t/h; D is screw outside diameter in m; d is centre-pipe outside diameter in m; P is pitch in m; n is screw speed in rpm; ρ is bulk density in t/m³; and φ is the assumed occupied fraction of the available annular area in this simplified model. The factor 60 converts minutes to hours. This is a geometric screening calculation, not a demonstrated delivery rate or a complete CEMA selection procedure. Actual slip, inclination, special flights and restrictions require verified allowance.
With P = D and a fixed ratio r = d/D, the model becomes:
D = ∛[Qm / (60 × (π/4) × (1 − r²) × n × ρ × φ)]
If d is fixed independently of D, this cube-root expression does not apply. Likewise, a loading percentage in a supplier’s table may use a different area convention; do not mix its factor with this annular model without confirmation. There is no universal 0.25–0.45 loading range for all cement and dry powders.
Illustrative calculation, not a product rating: assume 30 t/h, ρ = 1.2 t/m³, n = 100 rpm, φ = 0.30, P = D and r = 0.30. Required volume flow is 25 m³/h. Then:
D = ∛[30 / (60 × 0.7854 × 0.91 × 100 × 1.2 × 0.30)] ≈ 0.269 m
Ignoring the centre pipe would give about 0.260 m and overstate the available area. With D = 0.273 m and the same hypothetical ratios, the geometric result is about 31.4 t/h. That small difference from 30 t/h is not proof of adequate real capacity. Confirm actual pipe size, speed, loading, inclination and performance with the supplier before selecting the machine.
Standard diameter selection steps
- Define peak mass flow and the density states relevant to delivery and loading.
- Convert the required mass flow into volume flow using compatible units.
- Choose a loading and speed basis appropriate to the material and the correct feeder or conveyor duty.
- Screen possible geometry, then use the manufacturer’s matching tables or validated calculation method.
- Compare available sizes. VOGO lists Ø89, Ø114, Ø168, Ø219, Ø273, Ø323 and Ø407 mm; verify the dimensional definition and actual screw geometry.
- Check permissible screw speed for the material and construction. A table maximum is not a suitable operating speed for every powder. There is no single universal “critical rpm” at which all materials stop moving forward.
- Calculate running power and loaded-start torque, then verify the reducer, shaft, couplings and bearings. A 4-pole motor around 1,450 rpm is a motor reference, not the screw speed after reduction.
Inclination and layout adjustments
Inclination can increase fallback and alter filling, reducing useful capacity for a given configuration. The reduction is not a fixed loss per degree across all materials. Use data applicable to the actual angle, flight, tube or trough, speed and powder. If a validated design needs more capacity, compare a larger diameter, revised speed, shorter pitch or another arrangement rather than assuming one change always works.
Shortening pitch reduces geometric displacement at the same speed and loading, even when it improves material retention on an incline. Both effects must be evaluated together. Multiple inlets or outlets require checking flow and loading along each section, outlet sequencing and possible accumulation. See the capacity calculation guide for separating base geometry from operating corrections.
When engineering confirmation is required
Seek a specific engineering selection for the following conditions:
- Inclined duty, especially where the angle is outside the supplier’s validated range; 20° is not a universal threshold at which every design must change.
- Abrasive, sticky or agglomerated material requiring suitable construction, clearance and loading.
- A flooded inlet below a silo: the feeder’s withdrawal profile, inlet head load and hopper flow must be designed together. Increasing pitch, taper or another justified arrangement may be needed.
- Hot, moisture-sensitive or hazardous powders requiring appropriate thermal movement, seals, materials and containment.
- Intermittent feed, consolidation or loaded restart requiring adequate torque and overload protection.
- Long spans or nonstandard assemblies requiring shaft-deflection, support and bearing checks. A 15 m boundary is not a universal mechanical rule; VOGO’s listed length options extend from below 1 m to below 15 m.
Conclusion
Confirm a diameter against volume flow, operating speed, real geometry and layout, then separately verify strength, drive and startup. Keep the assumptions with the calculation so that a change in material or duty triggers a review. Catalogue capacity is a selection reference; obtain a project-specific confirmation using the complete material and installation data.