
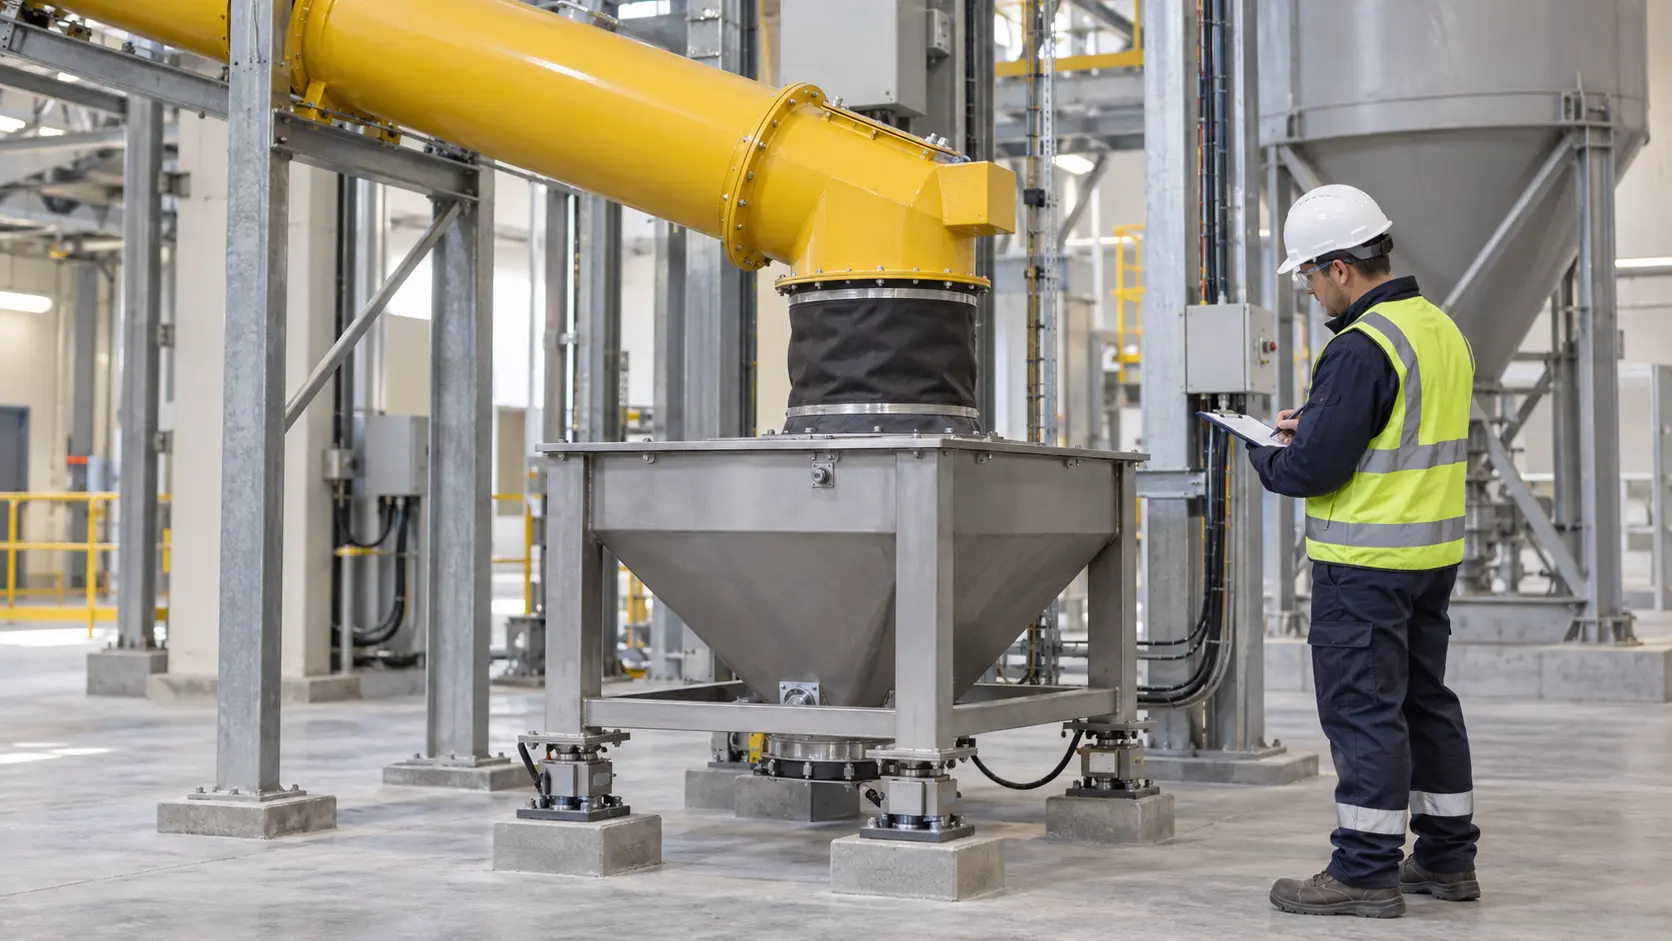
A cement screw conveyor flexible connection should keep cement inside the transfer while preventing the conveyor from carrying, lifting, or restraining a load-cell weigh hopper. The connector must be selected for the expected motion, material, temperature, pressure direction, and cleaning duty; installed in its neutral shape; and tested with the conveyor and dust-control system in every normal state. Calling a sleeve “flexible” does not prove that it is force-free.
The VOGO cement screw conveyor range is configured around each project’s material, route, duty, and interfaces. Published VOGO information does not specify a universal flexible connector, pressure rating, leakage class, or weighing accuracy. Those values belong in the project interface schedule and must be verified against the chosen hopper, load cells, connector, and ventilation system.
Define the weighing boundary before choosing a sleeve
Draw one boundary around every item whose mass the scale is intended to measure. The weigh hopper, its contents, mounted vibrator if used, discharge valve, and any equipment fixed to the hopper contribute to dead or live load. Fixed plant outside that boundary should not create a parallel load path through a chute, duct, cable, air line, platform, or connector.
The Rice Lake Load Cell and Weigh Module Handbook calls attached piping the largest source of error in vessel weighing. It explains that a vessel moves as its load cells and support structure deflect, and that an attached connection can react against that motion. Its piping guidance recommends flexible hose or bellows where possible, but says they must not be used to correct an initial offset. The practical lesson extends to dry-powder sleeves: align the equipment first, then use the connector to accommodate specified movement.
Classify the screw separately. If a valve or independent feeder meters cement into it, the machine operates as a control-fed conveyor. If its inlet is continuously open beneath a hopper, bin, or silo, it is flood-loaded and functions as a screw feeder. KWS’s feeder explanation makes the same distinction and describes variable-pitch flighting through the inlet. A feeder design may instead use increasing pitch, tapered outside diameter, or a mass-flow arrangement according to the withdrawal duty. A downstream flexible sleeve does not change that classification.
For flood-loaded duty, check head load, loaded starting torque, VFD low-speed torque, reducer service factor, and stall protection. Do not apply a normal control-fed conveyor capacity table to the inlet. The screw also cannot cure every arching or rat-holing problem; silo geometry, outlet dimensions, wall friction, moisture, consolidation, compaction, and flow aids remain system variables.
Specify the cement screw conveyor flexible connection
Ask the connector supplier to document the operating envelope rather than supplying “a flexible sock.” The minimum input set is:
| Input | What must be stated | Why it matters |
|---|---|---|
| Material | Cement type, temperature, moisture tendency, abrasiveness, and cleaning method | Controls fabric, coating, seam, and wear compatibility |
| Geometry | Bore, flange pattern, neutral face-to-face length, allowable axial and lateral movement | Prevents preload and contact through the hopper’s full travel |
| Pressure | Normal and upset differential pressure, vacuum or positive direction, and transients | Affects sleeve shape, leakage, apparent load, and failure mode |
| Weighing | Maximum permitted zero shift, batch error, load-cell capacity, and hopper movement | Turns “flexible” into a measurable acceptance requirement |
| Duty | Starts per hour, flow duration, vibration, filter-cleaning pulses, and inspection interval | Defines fatigue and test cases |
| Safety | Guarding, access, isolation boundaries, and retained material | Prevents maintenance access to moving or stored energy |
Install the connector with both mating flanges centered, parallel, and at the supplier’s neutral separation. A sleeve pulled tight can add downward or upward force as the hopper moves. One compressed into folds may buckle, abrade, trap cement, or touch nearby steel. Lateral offset, flange angularity, and twist create side load and make the sleeve stiffness unpredictable.
Support the conveyor, transition, extraction duct, cables, and pipes independently of the scale unless their mass is deliberately included in the weighing boundary. Give flexible cables a free loop without letting them rub the frame. Confirm clearance not only when the hopper is empty, but also when it is full, vibrating, thermally displaced, and undergoing its permitted restraint movement.
Material buildup can turn a compliant connector into a rigid bridge. Inspect the bore and folds for compacted cement, but do not solve buildup by choosing an excessively loose sleeve that collapses into the flow. The final geometry should keep the flow path open across the specified pressure and movement range.
Screen pressure-induced weighing error
Enclosed does not mean airtight or pressure-rated. A dust collector, fan, pneumatic transfer, filter-cleaning pulse, or displaced air from incoming cement can create pressure on the hopper and connector. HSE HSG258 treats the hood, duct, air cleaner, air mover, discharge, controls, and commissioning evidence as one local-exhaust system. The sleeve must therefore be evaluated as an interface within that system, not treated as the ventilation design itself.
A first-pass pressure-force screen is:
Force (N) = pressure difference (Pa) × effective area (m²)
Consider a hypothetical 200 mm effective diameter and a 200 Pa pressure difference:
- area = π × 0.20² ÷ 4 = 0.0314 m²;
- force = 200 × 0.0314 = 6.28 N;
- equivalent indicated mass = 6.28 ÷ 9.81 = 0.64 kg.
This is an illustrative screening calculation, not a VOGO performance value or a connector rating. A formed bellows or fabric sleeve may have an effective area different from its clear bore, and the pressure may also act on other hopper surfaces. Obtain the effective-area data and allowable differential pressure from the connector supplier, then verify the assembled system. If a 0.64 kg shift would consume too much of the batch tolerance, the interface or pressure control needs engineering attention before calibration.
Do not tune the scale to hide a state-dependent pressure force. Calibration made under one extraction condition can be wrong when the fan stops, a damper moves, or a filter pulse occurs. First stabilize the mechanical and air-pressure boundary; then calibrate and verify with traceable test loads or the approved material test.
Commission the connector with an operating-state matrix
An empty static check alone will miss many interface errors. Record a stable zero and repeatable test load through this sequence:
- conveyor and extraction off;
- extraction on at its normal setpoint;
- normal filter-cleaning cycle;
- conveyor running empty, where the process permits it;
- controlled cement transfer at minimum and maximum intended rates;
- hopper near its normal high and low working loads;
- discharge and refill transitions.
Use the same settling time and test load for comparisons. Observe the sleeve, but keep personnel outside guarded zones. Record differential pressure near the interface, hopper indication, conveyor state, airflow indicator, filter-cleaning state, material rate, and ambient or material temperature. Define pass/fail limits before the test.
The batch-overshoot diagnostic guide separates material afterflow from scale and cutoff effects. The venting and dust-control guide covers air boundaries, extraction inputs, and commissioning. For leakage at the drive or tail rather than the weigh-hopper interface, use the shaft-seal selection guide.
| Symptom | Likely interface question | Next safe check |
|---|---|---|
| Hopper zero changes when the fan starts | Is pressure acting over the connector or hopper effective area? | Compare pressure and indication with extraction off/on; inspect the ventilation balance |
| Indication shifts when the screw starts empty | Is vibration, torque reaction, cable restraint, or physical contact reaching the scale? | Check supports, clearances, cable loops, and adjacent vibration after safe isolation |
| Zero does not return after a batch | Has the sleeve changed shape or accumulated cement? | Empty, isolate, inspect folds and flange position, then repeat the test load |
| Sleeve bulges, collapses, or flutters | Is differential pressure outside its stated envelope? | Stop under the approved procedure and review pressure records and supplier limits |
| Dust leaks at a clamp | Are flange alignment, clamp load, fabric condition, and local pressure correct? | Isolate, clean, inspect, and correct the interface; do not assume extra clamp force is safe |
Before touching the connector, control all relevant energy and retained material. HSE machinery safety guidance says machinery should be switched off, isolated, or locked off before blockage removal, cleaning, or adjustment. A stop command or empty weight display is not proof that the screw, upstream material, pressure, or hopper valve is safe.
Procurement and acceptance checklist
Include these items in the purchase and commissioning record:
- interface drawing showing fixed and weighed boundaries, supports, flange coordinates, neutral gap, movement, and access;
- connector material, construction, dimensions, temperature range, pressure/vacuum envelope, movement limits, and replacement life basis;
- permitted mechanical-force or installed weighing-error contribution;
- load-cell capacities, restraints, cable routing, test-load method, and zero-repeatability criterion;
- normal and upset ventilation states, differential-pressure measurement points, alarms, and filter-cleaning sequence;
- screw classification as control-fed conveyor or flood-loaded feeder, plus drive and protection data;
- guarded access and the isolation method for the screw, upstream material, fan, pressure, vibrator, and hopper valve;
- witnessed results for static loads, fan on/off, empty running, cement transfer, filter pulses, refill, discharge, and zero return.
Facts in this guide come from the cited weighing, ventilation, machinery-safety, and feeder sources. The connector arrangement and acceptance limits above are engineering recommendations that must be confirmed for the project. VOGO product information is limited to the linked range page and is not evidence of weighing accuracy, airtightness, pressure rating, or a supplied connector.
Conclusion
A cement screw conveyor flexible connection succeeds only when it contains cement without bypassing the load cells. Define the weighing boundary, align the flanges before fitting the sleeve, specify material and movement limits, screen pressure force using the supplier’s effective area, and verify zero return across every conveyor and ventilation state. Treat any flood-loaded upstream screw as a feeder and keep its head-load and drive checks separate from the flexible-connection acceptance test.
For an interface review, send VOGO the layout, material duty, flange drawing, hopper and load-cell data, connector envelope, pressure cases, ventilation sequence, and permitted weighing error.