
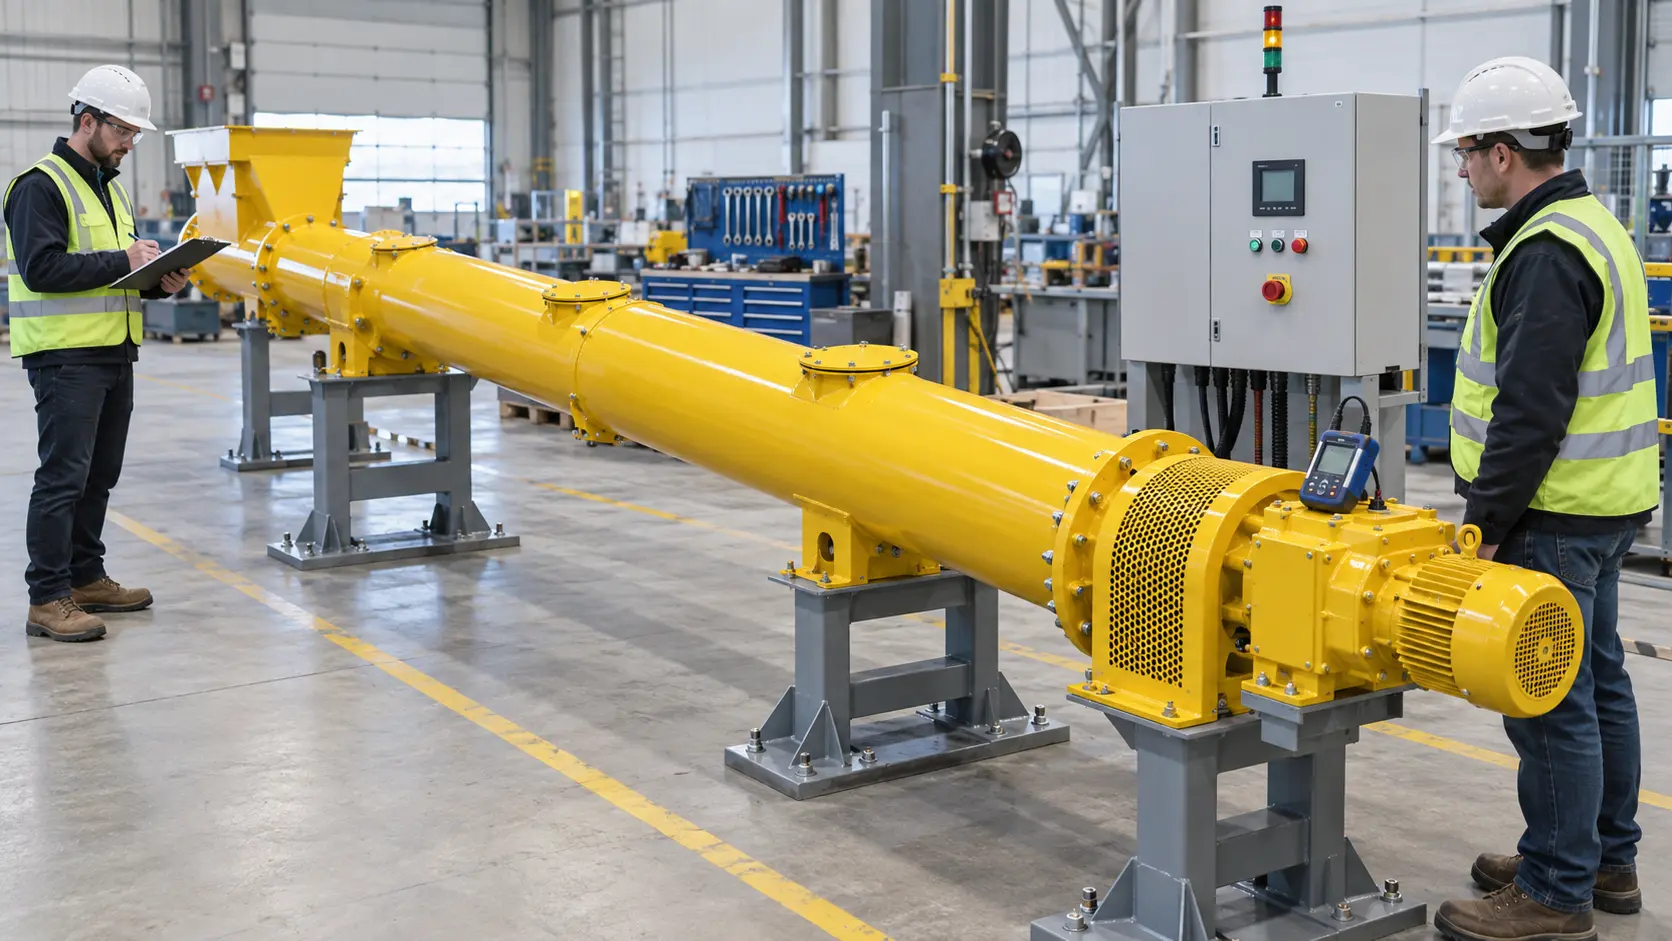
Cement screw conveyor FAT and SAT should not be one generic “run test.” Create an approved inspection and test plan before manufacture ends. For every check, state the requirement, factory or site location, operating condition, method, calibrated instrument, acceptance limit, witness, evidence, and action if it fails. FAT verifies what can be proven before shipment; SAT proves the installed conveyor, interfaces, controls, material duty, and safety functions under site conditions.
The VOGO cement screw conveyor range is configured for a project’s material, duty, route, and interfaces. Its published information does not define universal FAT or SAT limits for capacity, vibration, noise, leakage, temperature, power, or restart. The purchase specification, approved drawings, component manuals, applicable standards, and agreed test plan must supply those criteria.
Set the acceptance basis before testing
Start with a requirements matrix, not a supplier’s standard tick sheet. Each purchase-order requirement should point to an inspection, calculation, certificate, test, or site demonstration. Mark who reviews, witnesses, and approves it. Identify hold points that prevent painting, closing the casing, shipment, energization, material introduction, or handover.
ISO 12100 provides a methodology for machinery risk assessment and risk reduction across relevant life-cycle phases and calls for documentation and verification of the process. It does not supply a ready-made screw conveyor checklist. Use the project risk assessment to decide which guards, interlocks, isolation provisions, warnings, access controls, and residual-risk instructions require evidence at FAT and SAT.
Separate three kinds of statement in the test plan:
| Statement type | Example | Acceptance basis |
|---|---|---|
| Verifiable requirement | Motor nameplate shall match the approved data sheet | Drawing, data sheet, purchase order, or applicable standard |
| Project engineering decision | Loaded restart must be demonstrated after the agreed stop condition | Approved duty and test procedure |
| Supplier information | Offered conveyor diameter, motor, reducer, and interfaces | Approved VOGO submittal for that order only |
Do not convert an engineering recommendation into a claimed legal requirement. Applicable electrical and machinery rules vary with destination, system boundary, and contract. The purchaser should identify the required edition and jurisdiction before design approval.
Define what FAT can and cannot prove
Factory acceptance is most useful while defects can still be corrected before packing. It can verify identity, dimensions, workmanship, accessible internals before closure, component data, guarded assembly, electrical logic, and a controlled no-load run. It cannot normally prove the final foundation, field cable routing, upstream material behavior, downstream restriction, installed dust extraction, or sustained capacity with the customer’s cement.
A practical FAT sequence is:
- review approved drawings, bill of materials, material certificates where specified, motor and reducer data, weld and coating records, and deviations;
- verify overall dimensions, inlet and outlet orientation, supports, access covers, lifting points, rotation arrow, guards, labels, and flange interfaces;
- inspect the screw, casing, end bearings, intermediate supports, seals, fasteners, and internal clearances before final closure where the inspection plan permits;
- confirm lubricant type and level, coupling alignment record, reducer mounting, fastener status, and manual rotation under the approved isolated procedure;
- test the panel, local controls, direction command, permissives, alarms, speed feedback, emergency stops, and shutdown sequence;
- run empty for the agreed duration and record speed, current, bearing and reducer temperatures, vibration points, noise observations, contact, leakage, and abnormal movement;
- close punch items and compile signed evidence before release.
IEC 60204-1 is the international reference for electrical equipment of machines covered by its scope. The project electrical test must be prepared by a competent electrical engineer using the applicable edition, supply system, protection scheme, and local rules. A powered functional demonstration does not replace the required inspection, continuity, protection, insulation, documentation, or verification work.
The CEMA No. 352 publication listing identifies its screw conveyor safety, operation, and maintenance manual. Use the purchased manual and supplier instructions to establish conveyor-specific safety practices and labels. A CEMA logo, component dimension, or generic checklist is not evidence that a complete machine complies with every project requirement.
Make no-load FAT measurements repeatable
Record the test state so the result can be reproduced. Minimum context includes supply voltage and frequency, VFD output frequency, motor speed, reducer ratio, screw speed, rotation direction, ambient temperature, run duration, lubrication state, support arrangement, and measurement locations. A photo of a running machine without these details is not an acceptance record.
Define measurement points on stationary motor, reducer, and end-bearing housings. ISO 20816-1 establishes general conditions and procedures for measuring and evaluating machine vibration, including magnitude and change, but the correct standard part, machine class, mounting, quantity, location, and limit must be selected for the equipment. Do not paste a universal vibration value into the FAT plan for every motor, gearbox, casing, and slow screw shaft.
Compare no-load motor current with the drive data and with each phase where applicable, but do not invent a fixed percentage of nameplate current as a pass limit. Check for stable current, correct direction, unexpected load, rubbing, and repeatability using the motor and VFD manufacturers’ criteria. Likewise, temperature should be logged as a trend from a known start condition and judged against component instructions, ambient conditions, lubricant, load, and agreed duration.
If the factory cannot reproduce the final supports, note the temporary arrangement and reserve installed vibration and alignment acceptance for SAT. Passing on shipping stands does not prove that the site steelwork will be stiff, level, or free of transmitted vibration.
Use SAT to prove the installed system
SAT begins after installation records are complete, not when cement is first admitted. Verify foundations and steelwork, support spacing, casing centerline, flange alignment, expansion provisions, drive alignment, fasteners, lubricant, guards, access, flexible connections, earthing, field wiring, cable protection, rotation, and instrument calibration.
The cement screw conveyor installation and alignment guide provides detailed mechanical hold points. The VFD control and protection guide covers permissives, speed proof, trips, and sequencing. For measurement routes and interpretation limits, use the vibration troubleshooting guide rather than repeating generic limits here.
HSE’s machinery safety guidance says machinery should be complete, stable, guarded, maintained, and properly isolated or locked off before blockage removal, cleaning, or adjustment. SAT should therefore prove normal operation and foreseeable interventions: emergency stopping, restart prevention, isolation boundaries, access to routine service points, and control of retained material. An emergency stop is not an energy-isolation device.
Before loaded testing, prove the empty sequence from downstream to upstream start and upstream to downstream stop as required by the process. Simulate each agreed fault without creating a hazard: loss of downstream permissive, speed feedback, guard interlock where fitted, dust extraction, high current or torque signal, and upstream feed. Record the commanded action, actual response, alarm, reset condition, and prevention of an automatic unsafe restart.
Classify the inlet before the loaded test
The inlet condition determines the duty. A valve or separate feeder that controls inflow makes the screw a control-fed conveyor. A continuously open hopper, bin, or silo over the inlet flood-loads the screw, so it performs as a screw feeder. The second case needs withdrawal uniformity, head load, full-start torque, VFD low-speed torque, reducer service factor, stall protection, and silo-flow behavior in the acceptance plan.
For feeder inlets, variable or increasing pitch, tapered outside diameter, or a designed mass-flow arrangement may be used according to the application. “Reduced pitch” alone is not a complete withdrawal design. A normal control-fed capacity table must not be used as proof of flood-loaded feeder output.
Neither FAT nor SAT should claim the screw prevents all arching, rat-holing, or bridging. Hopper geometry, outlet size, wall friction, moisture, compaction, consolidation, aeration, and flow aids affect discharge. If the material does not reach the screw consistently, record that system condition rather than forcing the conveyor to carry the blame or declaring an unsupported capacity failure.
Run a defined loaded-duty scenario
A capacity test needs mass, time, material condition, and operating state. Use a calibrated scale, weigh hopper, or other agreed method. For a hypothetical test, suppose 6,000 kg is transferred in 12 minutes after excluding startup and shutdown transients:
Measured rate = 6,000 kg ÷ (12 ÷ 60) h = 30,000 kg/h = 30 t/h
This arithmetic example is not a VOGO capacity claim. The record must also state cement type, measured bulk density, moisture condition, screw speed, inclination, inlet control, fill condition, run length, current, temperature, downstream state, and measurement uncertainty. Compare the result only with the contractual duty at the defined conditions.
Test the agreed minimum, normal, and maximum rates long enough to reach meaningful thermal and process conditions. If the contract requires loaded restart, define how the machine is stopped, how long material rests, silo level, inlet condition, restart speed or VFD mode, maximum allowable torque or current, confirmation time, and abort criteria. Repeated resets after a stall are not an acceptance method.
Enclosed does not mean airtight or pressure-rated. Inspect dust release at flanges, covers, seals, flexible connectors, and transfer points under the specified ventilation state, but use a stated leakage or exposure criterion. Do not record “no dust” merely because none is visible. Positive or negative pressure capability must be supported by the housing, seal, connector, and system design.
Control failures, punch items, and conditional release
Use four result states: pass, fail, not tested, and accepted deviation. “Not tested” must identify why, who owns the later test, and the new hold point. An accepted deviation needs written technical disposition and purchaser approval; it is not the same as a pass.
| Finding | Correct disposition |
|---|---|
| Nameplate or dimensions differ from approved data | Stop and resolve configuration before functional testing |
| Abnormal rub, impact, rapid heating, or unstable current | Stop safely, isolate, investigate, repair, and repeat the affected test |
| Interlock acts opposite to the cause-and-effect chart | Block release; correct logic through controlled change and retest all affected paths |
| Capacity test lacks bulk density or mass traceability | Mark not proven and repeat with an approved measurement method |
| Dust release occurs only when extraction is unavailable | Resolve the ventilation permissive and containment boundary; do not call the housing airtight |
| Required loaded restart is not safe to reproduce at the factory | Reserve it explicitly for SAT with an approved site procedure |
After a repair or software change, repeat the failed check and every dependent test. Record the revision, person authorizing the change, as-left settings, and objective evidence. Closeout should include signed test sheets, calibrated-instrument identification, photos where useful, drawings, data sheets, certificates required by contract, software and parameter backups, lubrication schedule, spare-parts list, residual-risk information, and operator and maintenance instructions.
Conclusion
Cement screw conveyor FAT and SAT are effective when every result is tied to an approved requirement and a reproducible operating state. Use FAT for manufacture, guarded assembly, controls, no-load behavior, and documentation; use SAT for installed alignment, interfaces, safety functions, dust control, loaded capacity, and restart cases. Preserve the feeder/conveyor distinction, define limits before testing, and never let an incomplete or failed hold point become an undocumented pass.
For a project test-plan review, send VOGO the duty, layout, inlet condition, control narrative, component data, required standards, acceptance limits, witness points, and document list.
References
ISO 12100:2010 Safety of Machinery — Risk Assessment and Risk Reduction ↗IEC 60204-1:2016+AMD1:2021 Electrical Equipment of Machines ↗ISO 20816-1:2016 Mechanical Vibration — General Guidelines ↗CEMA No. 352 Screw Conveyor Safety Operation and Maintenance Manual ↗HSE Introduction to Machinery Safety ↗